EN
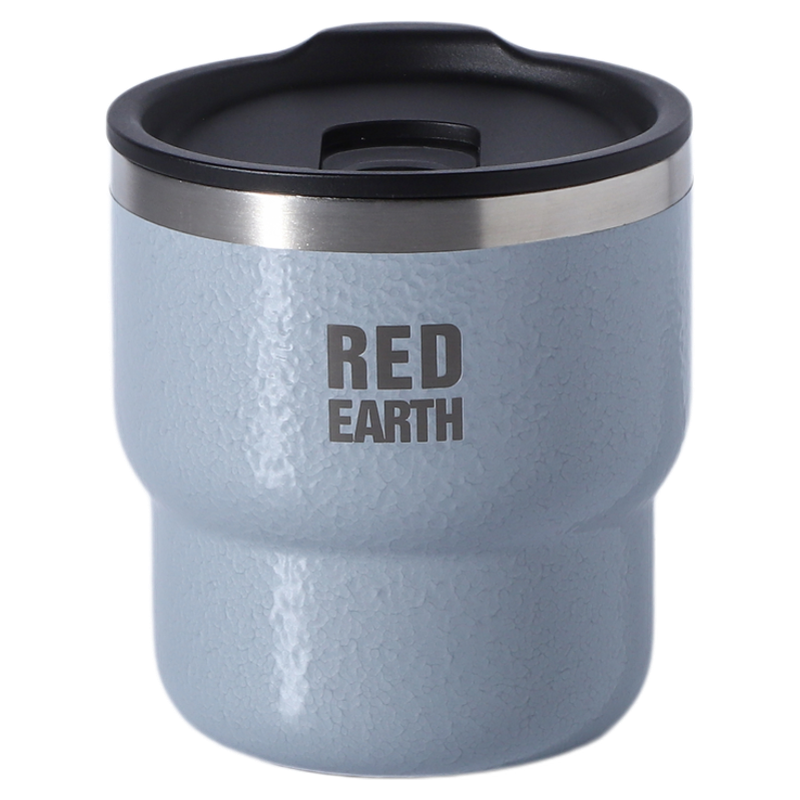
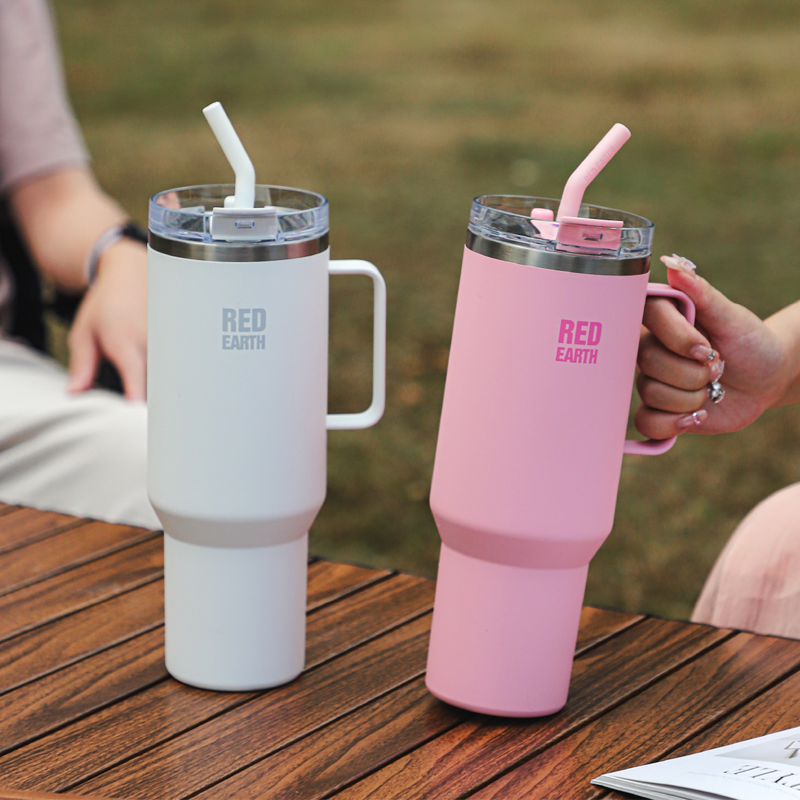
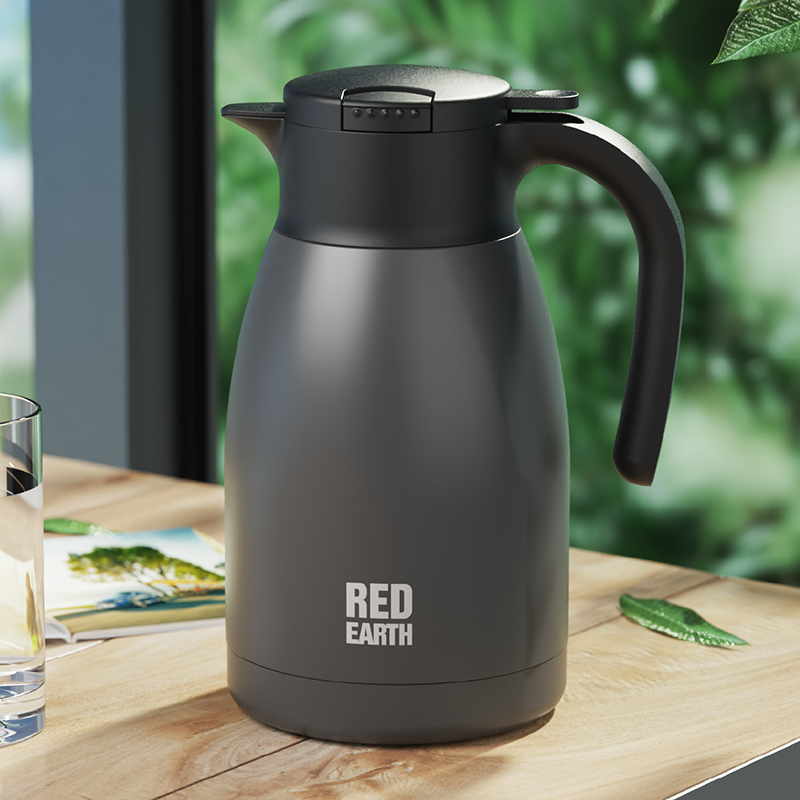
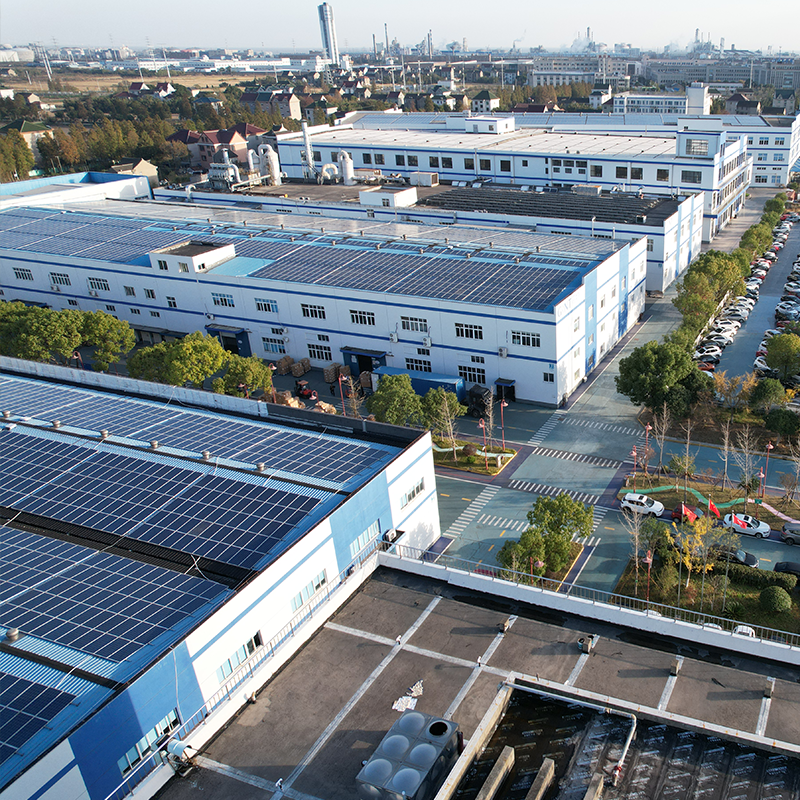
The double insulated drink bottle has become an essential item for consumers seeking to maintain beverage temperatures over extended periods. At Zhejiang Gint Vacuum Flask Technology Co., Ltd., we specialize in manufacturing these bottles with unmatched precision and quality. Our advanced double-wall insulation consists of two stainless steel layers separated by a vacuum, effectively reducing heat transfer through conduction and convection. This design ensures that hot beverages remain hot for up to 12 hours and cold beverages stay chilled for up to 24 hours, making our bottles ideal for travel, sports, and daily commutes. Our manufacturing facility is ISO-certified, reflecting our dedication to quality management and continuous improvement. We employ state-of-the-art production lines that integrate automated welding, leak testing, and vacuum extraction to create a reliable vacuum seal. Each bottle is subjected to rigorous quality control checks, including thermal performance tests, leak-proof tests, and durability inspections, ensuring that every product meets global standards. Customization is a cornerstone of our service. We offer a wide range of capacities, from 350ml to 1500ml, and a variety of mouth diameters to accommodate different drinking needs. Our finishing options include powder coating, matte, or glossy textures, plus we provide custom logos and packaging. This flexibility allows businesses to create a unique product that stands out in a competitive market. Additionally, our double insulated drink bottles are made from food-grade 304 stainless steel, ensuring safety and resistance to corrosion. The materials and manufacturing processes are compliant with international regulations, including FDA and LFGB standards. We also consider environmental impact; our products are reusable and contribute to reducing single-use plastic waste, aligning with consumer awareness of sustainability. With over a decade of experience, we continue to innovate and adapt to market trends. Our engineering team can assist in developing specialized solutions, such as infuser baskets, smart temperature indicators, or carb-free coatings. We partner with brands across sectors—outdoor gear retailers, corporate wellness programs, and promotional product distributors—providing reliable supply chain support and scalable production. Request a quote today to discover how our double insulated drink bottles can enhance your product portfolio and satisfy discerning customers worldwide.
20
Jul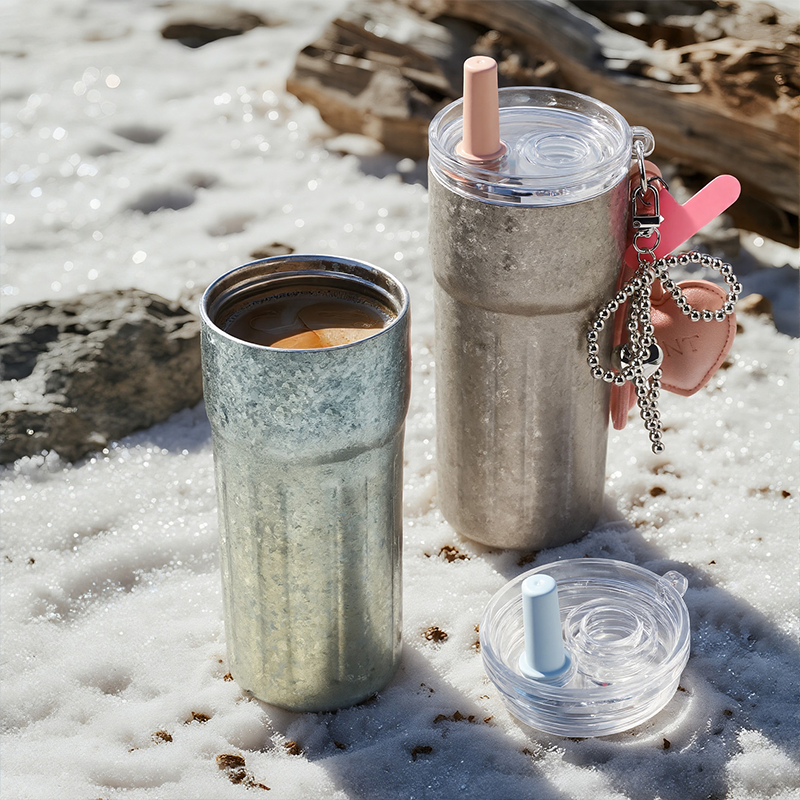
08
Jul
11
Aug
13
Aug