EN
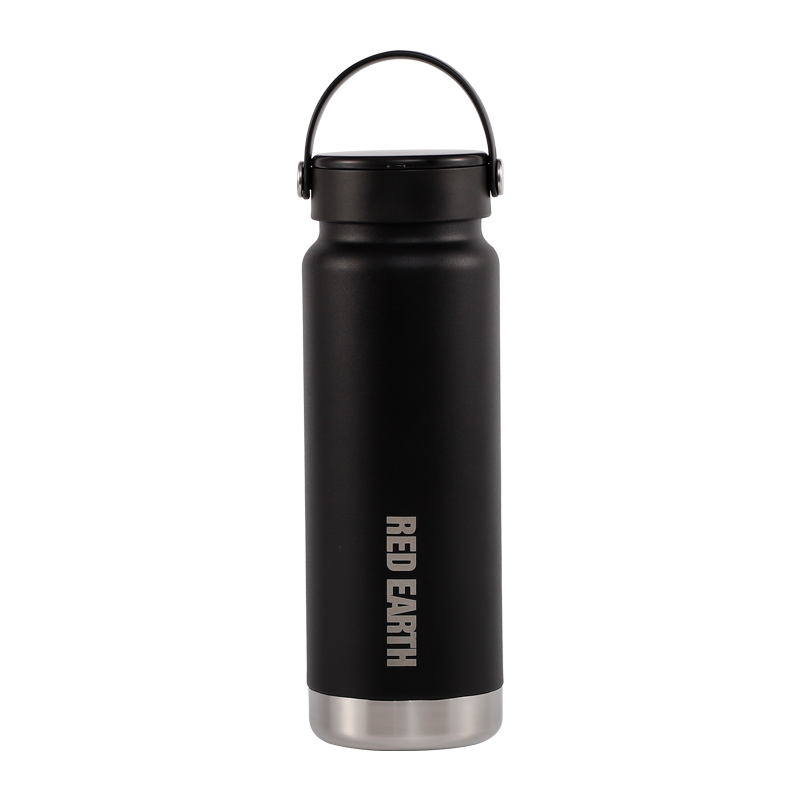
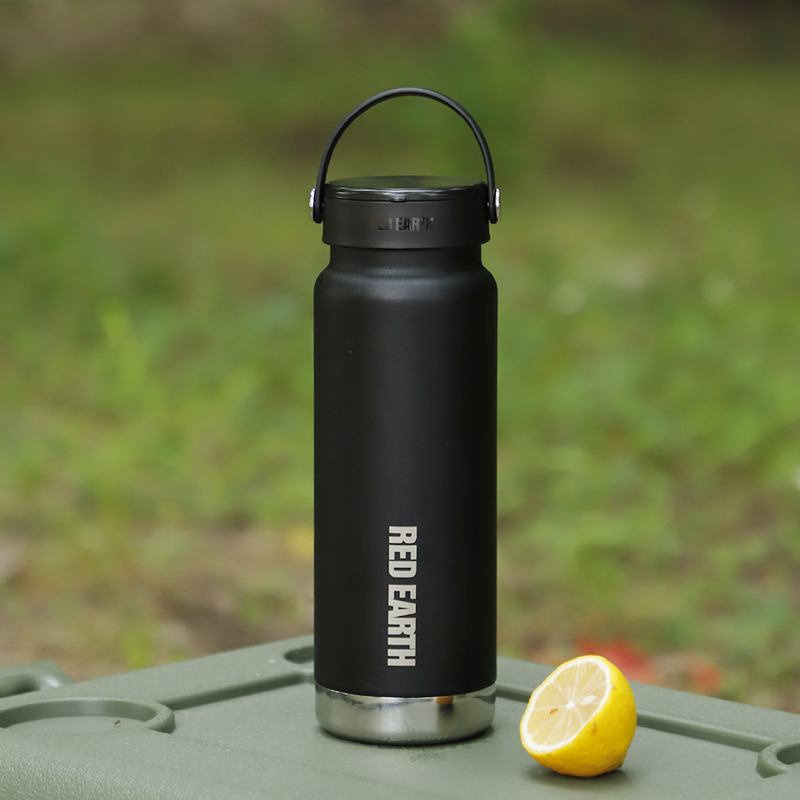
**The Science of Thermal Retention: Why Our Thermal Drink Bottle Outperforms Others** In the realm of insulated drinkware, the term “thermal drink bottle” encompasses a critical technology that directly impacts user experience: the ability to maintain a desired beverage temperature for extended periods. At Zhejiang Gint, we elevate this concept through materials science and precision engineering. The core of our thermal drink bottle lies in the vacuum insulation layer, which eliminates air molecules between the inner and outer stainless steel walls, effectively preventing thermal transfer. This vacuum creates a barrier that is nearly impossible for heat to traverse, whether from the environment to your iced drink in summer, or from your hot coffee to the outside in winter. But achieving a true vacuum is only the beginning. Our bottles undergo a multi-step production process that includes electrolysis polishing to smooth microscopic imperfections, which reduces surface area for heat transfer and enhances corrosion resistance. The outer layer is treated with a thermal reflection coating to further inhibit radiant heat loss. We also employ a specialized copper foil layer in the vacuum space for select models, which mirrors radiant heat back into the beverage, boosting hot retention by up to 20%. Another critical factor is the closure system. The cap is a common point of heat loss; therefore, we have engineered a double-wall cap with a trap that retains heat, and a silicone seal that forms a hermetic closure, preventing any air exchange. Our thermal drink bottle is tested in a controlled environment where temperature is recorded at multiple intervals over 48 hours, and the results demonstrate a temperature loss of less than 5°C over 12 hours for hot liquids. This performance meets the stringent requirements of industrial users, such as field workers who need hot beverages during long shifts, and commercial sectors like hospitality, where serving consistency is paramount. Beyond performance, we address the growing demand for sustainability. Our thermal drink bottles are reusable, reducing single-use plastic waste. The 316 stainless steel is 100% recyclable, and the powder coating is free from BPA, phthalates, and lead. By choosing our thermal drink bottle, you not only invest in a durable product but also contribute to a greener planet. For businesses, an private label or custom branded thermal drink bottle serves as a constant reminder of your brand’s commitment to quality and sustainability. It is an effective marketing tool that offers practical value, ensuring high frequency of use and brand visibility. Our engineering team is dedicated to continuous improvement, exploring advanced materials like phase-change materials for future models that can even heat beverages without external power. In an era where consumers are becoming increasingly discerning about product quality and environmental impact, our thermal drink bottle represents the gold standard. Whether you are a procurement manager for an outdoor equipment chain, a marketing executive seeking promotional gifts, or a retailer looking for high-margin products, our thermal drink bottle offers a compelling value proposition. We provide comprehensive technical support, including product specification sheets, certification documents, and performance test reports, to help you make informed decisions. Contact us to discuss your requirements and discover how our thermal drink bottle can elevate your product lineup.
20
Jul
08
Jul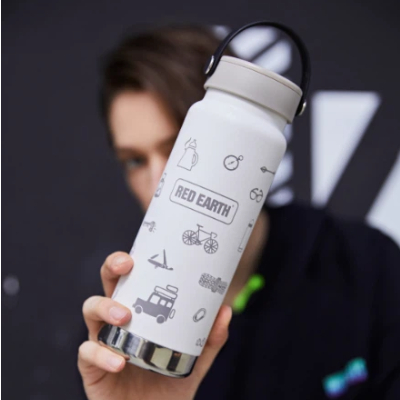
24
Jul
11
Aug